MDO-PE Films in Recyclable Packaging: The Engineering Guide
For decades, consumer flexible packaging relied almost exclusively on multi-material laminates. To achieve shelf-life stability, mechanical stiffness, and print brilliance, converters bonded chemically incompatible polymers together: BOPET (Biaxially Oriented Polyethylene Terephthalate) for thermal stability and reverse printing, BOPA (Nylon) for puncture resistance, Aluminum Foil for gas barriers, and LLDPE (Linear Low-Density Polyethylene) as the heat-sealable inner liner.
While these structures excel at product preservation, they are virtually impossible to recycle mechanically. Because PET melts at roughly 255°C and PE at 120°C, reprocessing mixed films in mechanical extruders causes thermal phase separation, generating contaminated, brittle plastic regrind with zero commercial value.
With the enforcement of the European Union Packaging and Packaging Waste Regulation (EU PPWR), UK Plastic Packaging Tax (PPT), and global circular economy commitments (CEFLEX and RecyClass guidelines), consumer brands face mandatory targets to transition from multi-material laminates to Mono-Material Polyethylene (Mono-PE, Resin Identification Code #4).
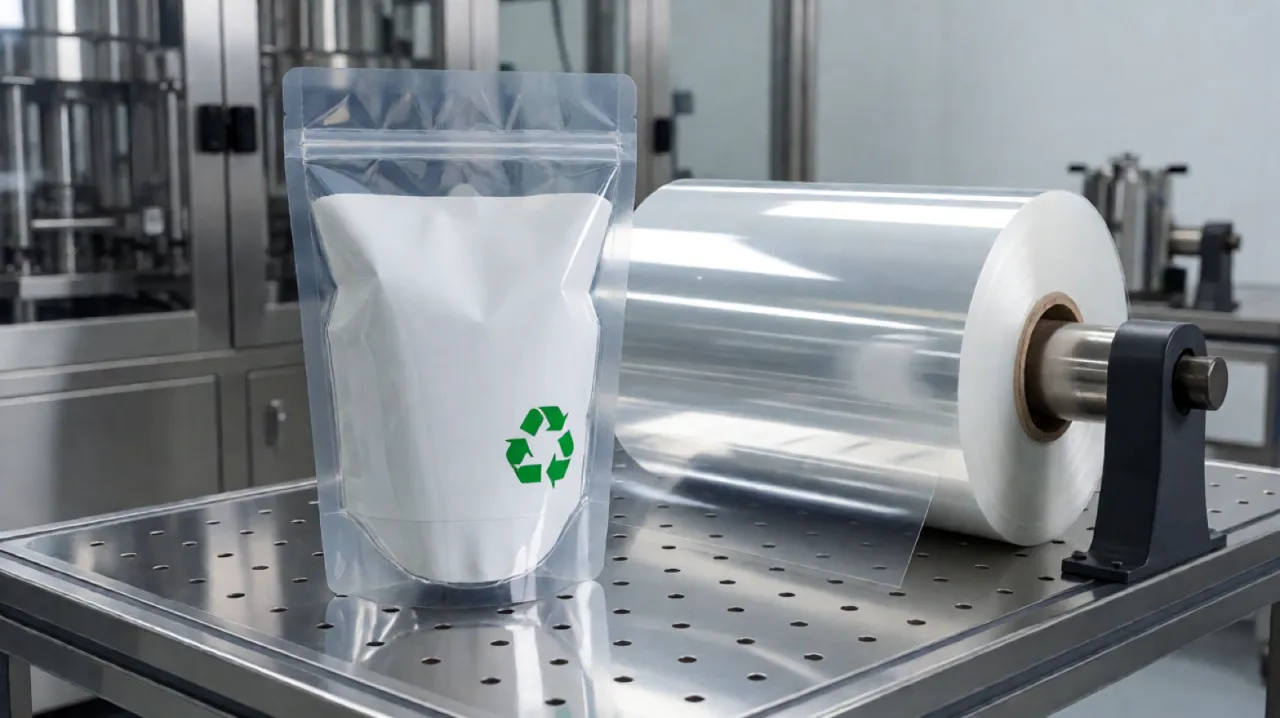
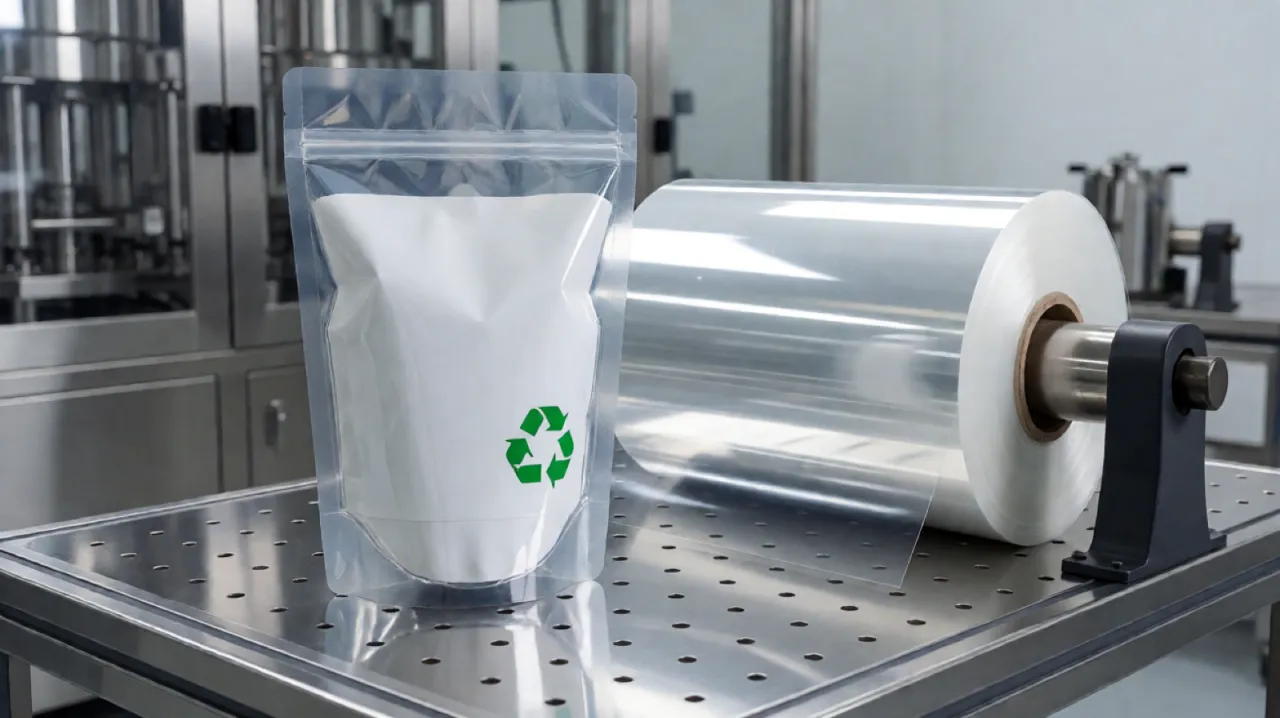
The primary technological breakthrough enabling this shift without sacrificing pouch stiffness, optical transparency, or filling machine speed is Machine Direction Oriented Polyethylene (MDO-PE).
This engineering guide outlines the polymer physics, barrier integration, converting protocols, and commercial realities of MDO-PE in recyclable flexible packaging.
The Physics of Machine Direction Orientation (MDO)
Standard blown or cast polyethylene film exhibits isotropic molecular chain entanglement interspersed with random crystalline lamellae spherulites. In this unoriented state, PE possesses high elongation (300%–600%) but low tensile modulus, making it too stretchy to maintain register on high-speed rotogravure printing presses and too soft to withstand hot heat-sealing jaws without burning through.
The MDO process transforms polyethylene from a pliable sealing web into a stiff, thermally resilient printing substrate through controlled uniaxial stretching:
The Machine Direction Orientation (MDO) Process:
┌─────────────────┐    ┌─────────────────┐    ┌─────────────────┐    ┌─────────────────┐
│ 1. Pre-Heating  │ ──>│ 2. Uniaxial     │ ──>│ 3. Annealing    │ ──>│ 4. Chill Roll   │
│    (95°C – 118°C│    │    Stretching   │    │    Relaxation   │    │    Quenching    │
│    Below Tm)    │    │    (4:1 to 8:1) │    │    Stress Relief│    │    Freeze State │
└─────────────────┘ └─────────────────┘ └─────────────────┘ └─────────────────┘- Pre-Heating Phase: Primary cast or blown PE film passes over heated oil-filled rollers (typically 95°C to 118°C), elevating the polymer chain mobility just beneath its crystalline melting temperature ($T_m$).
- Differential-Speed Stretching Phase: The heated web enters a narrow gap (often 1 mm to 3 mm) between two nip rollers. The second roller rotates at 4 to 8 times the rotational velocity of the first roller. Under high tensile draw, the crystalline spherulites unravel, forcing molecular polymer backbones to align strictly parallel along the machine direction.
- Annealing (Relaxation) Phase: The stretched film passes over intermediate conditioning rollers at slightly lower temperatures. This relieves internal frozen mechanical stress and realigns the crystalline lattice, reducing post-converting thermal shrinkage.
- Chill Roll Quenching: Water-cooled rollers instantly lock the oriented crystalline morphology into place, finalizing the film caliper (typically drawn down from 120–200 $\mu\text{m}$ to an ultra-thin 20–30 $\mu\text{m}$).
Technical Performance: MDO-PE vs. BOPET vs. Standard Blown PE
By ordering the polymer chains along the machine direction, MDO-PE approaches the mechanical stiffness and optical performance of traditional polyester (BOPET) while remaining 100% compatible with PE recycling streams:
| Physical Property | Standard Blown PE Film (50 $\mu\text{m}$) | MDO-PE Oriented Film (25 $\mu\text{m}$) | Biaxially Oriented PET (BOPET 12 $\mu\text{m}$) |
|---|---|---|---|
| Tensile Modulus MD (MPa) | 350 – 500 | 1,800 – 2,400 | 3,800 – 4,500 |
| Tensile Strength MD (MPa) | 35 – 55 | 180 – 260 | 200 – 250 |
| Elongation at Break MD (%) | 350 – 550% | 35 – 60% | 100 – 130% |
| Optical Haze (%) | 12 – 18% (Cloudy) | 1.8 – 3.5% (High Clarity) | 1.5 – 2.5% (Glass Clear) |
| Gloss at 60° (GU) | 55 – 70 | 110 – 135 | 130 – 150 |
| Thermal Shrinkage at 100°C | > 15% | < 2.5% | < 1.5% |
| Mechanical Recyclability | PE Stream #4 | PE Stream #4 (Fully Compatible) | Mixed Plastics (Incineration / Landfill) |
Solving the Heat-Sealing Window Challenge
In conventional BOPET/PE laminates, heat sealing is straightforward: the external BOPET layer does not soften until 250°C, while the internal PE sealant melts at 115°C. Packaging lines can set sealing jaws at 160°C–180°C with zero risk of melting the exterior web.
In an all-PE structure, however, both the outer print layer and the inner sealant layer are polyethylene. Without engineering, heated sealing jaws melt straight through the entire laminate, sticking to the metal bars and destroying pouch seals.
MDO-PE resolves this through differential thermal crystallization:
All-PE Sealing Architecture:
┌──────────────────────────────────────────────┐
│ MDO-PE High-Density Outer Web (Tm ~135°C)    │ ◄- Thermally Resistant Face
├──────────────────────────────────────────────┤
│ Solventless Polyurethane Adhesive Layer      │
├──────────────────────────────────────────────┤
│ Metallocene Low-SIT Cast PE Sealant (Tm ~95°C│ ◄- Melts & Hermetically Seals
└──────────────────────────────────────────────┘- MDO-PE Outer Layer: High-density orientation elevates the effective thermal deformation threshold up to 135°C – 140°C under short dwell times.
- Low-SIT (Seal Initiation Temperature) Inner Layer: Formulated using advanced metallocene or plastomer polyethylene resins that melt and form hermetic bonds at 90°C to 105°C.
- The Operational Window: This differential provides a workable 30°C to 40°C temperature processing window on form-fill-seal (VFFS/HFFS) lines, enabling high-speed packing without exterior blistering or jaw burn-through.
To explore recyclable pouch formats utilizing this architecture, review our stand-up pouches and flat bottom bags collections.
High-Barrier Solutions for Mono-PE Laminates
Pure polyethylene provides an excellent water vapor barrier (WVTR) but is naturally porous to atmospheric gases (Oxygen Transmission Rate typically exceeds $1,500\text{ cc/m}^2/\text{day}$). Delicate foods like roasted coffee, fatty snacks, and dry pet food require oxygen barriers below $1.0\text{ cc/m}^2/\text{day}$.
Converters deploy three circular-compliant barrier technologies that maintain mono-material recycling certification:
- Co-Extruded EVOH Barrier (< 5% Weight Fraction):
- Ethylene Vinyl Alcohol (EVOH) co-extruded as a central barrier core during primary film blowing before MDO stretching.
- Under both CEFLEX and RecyClass standards, EVOH content under 5.0% of total packaging weight is fully tolerated in mechanical PE recycling without compromising recycled pellet melt flow or mechanical integrity.
- Vacuum AlOx / SiOx Ceramic Deposition:
- Nanometer-thin layers of Aluminum Oxide ($AlO_x$) or Silicon Oxide ($SiO_x$) deposited onto corona-treated MDO-PE in high-vacuum plasma chambers.
- Provides glass-like optical transparency (ideal for product view windows) while driving OTR below $1.0\text{ cc/m}^2/\text{day}$ and WVTR below $1.0\text{ g/m}^2/\text{day}$.
- Vacuum Metallized MDO-PE (Met-MDO-PE):
- Vacuum aluminum vapor deposition onto MDO-PE film, delivering near-zero gas permeability and complete UV light shielding, effectively replacing conventional metallized polyester (VMPET).
For comprehensive regulatory compliance frameworks, see our EU PPWR sustainable packaging guide and sustainable mono-material recyclable pouches guide.
Printing and Converting Best Practices
Converting MDO-PE requires adjusted press tension and web handling protocols compared to traditional BOPET:
- Tension Control: While MDO-PE exhibits high tensile modulus in the machine direction (MD), its transverse direction (TD) tear strength is lower due to uniaxially aligned fibrils. Rotogravure and central-impression flexographic presses must maintain strict closed-loop web tension to avoid web neck-in or wrinkles.
- Surface Treatment Retention: MDO-PE requires inline corona treatment during printing to maintain dyne levels at $\ge 42\text{ dynes/cm}$ for robust ink anchorage.
- Recyclable Inks and Adhesives: Solventless two-component polyurethane laminating adhesives certified under RecyClass protocols ensure that cured adhesives do not cause discoloration during post-consumer flake wash and thermal re-pelletization.
Commercial Procurement Specification Matrix
| Metric | Standard MDO-PE Clear Web | High-Barrier EVOH MDO-PE | Metallized Met-MDO-PE | Ceramic AlOx Transparent Barrier |
|---|---|---|---|---|
| Standard Caliper | 20 – 30 $\mu\text{m}$ | 25 – 35 $\mu\text{m}$ | 20 – 30 $\mu\text{m}$ | 25 – 30 $\mu\text{m}$ |
| OTR ($\text{cc/m}^2/\text{day}$) | ~1,200 (Moisture only) | < 1.5 | < 0.5 | < 1.0 |
| WVTR ($\text{g/m}^2/\text{day}$) | < 2.0 | < 1.5 | < 0.3 | < 0.8 |
| Optical Clarity | High Clarity Gloss | High Clarity Gloss | Opaque Metallic Silver | Transparent Clear Barrier |
| Recycle Stream | PE Stream #4 | PE Stream #4 (<5% EVOH) | PE Stream #4 (Micro-metal) | PE Stream #4 |
| Primary Application | Confectionery & Dry Pasta | Coffee & Pet Treats | Roasted Coffee & Nuts | Organic Cereals & Snack Bars |
The Road Ahead for Circular Flexible Packaging
Transitioning to MDO-PE mono-material flexible packaging allows brand owners to eliminate multi-material landfill waste, insulate operations against escalating European plastic taxes, and display genuine circular economy credentials without compromising barrier shelf life.
To evaluate MDO-PE film samples, test oxygen barrier transmission rates, or develop custom recyclable pouch laminates for your product line, contact the materials engineering team at the CraftPack Global Contact Team.